A packaging sample can look ready for production without proving that the package is ready for production. One carefully made sample may have a clean surface, smooth opening action, and apparently accurate fit, yet commercial manufacturing introduces dimensional variation, material variation, forming differences, and process tolerances that a single sample cannot represent. This distinction is particularly important for a paper round box because a cylindrical structure depends on the relationship between circular geometry, wall formation, lid-to-body clearance, bottom construction, and the packed product. A small change in diameter can affect opening resistance, slight ovalization can change lid alignment, and product weight can alter how loads pass through the insert and into the bottom of the box.
For brands developing round gift boxes or other rigid box packaging, approval should therefore progress from specification to geometry, from geometry to function, and from function to repeatability. Buyers evaluating custom round boxes should not focus only on whether one sample looks correct. A stronger approval process determines whether the characteristics that make that sample successful have been defined clearly enough to be measured, reproduced, and controlled during production.
Define What the Sample Is Actually Approving
Before physical testing begins, the buyer and manufacturer need to establish what the sample is intended to represent. An early structural sample may confirm diameter, height, opening sequence, insert concept, and product positioning, while a later pre-production sample may additionally represent the intended board, printed wrapping paper, finishing, adhesive construction, and assembly method. These samples provide different levels of evidence, so an approval should apply only to the characteristics that the particular sample can genuinely demonstrate.
This distinction becomes especially important when handmade samples are used. A carefully prepared handmade sample can be suitable for confirming dimensions, structure, appearance, or product positioning, depending on how it was produced, but it cannot automatically validate characteristics that depend on production tooling or repetitive manufacturing processes. Final circularity may be influenced by forming equipment; foil registration may depend on production tooling; wrapping consistency may be affected by adhesive application, positioning, machine settings, and operator control. In custom rigid box packaging, a highly refined handmade sample can therefore look better than the variation that will naturally appear once the same construction is produced repeatedly.
The approval basis should identify the structural drawing revision, material specification, artwork version, insert configuration, intended product, and any known differences between the sample and the proposed production construction. Establishing this reference first prevents later measurements from being applied to a sample that no longer represents the actual manufacturing specification.
Verify Geometry Before Judging the Opening Experience
Once the approval basis is fixed, geometric verification should come before subjective evaluation of the opening experience. The reason is mechanical: the lid can only perform consistently if the body geometry with which it engages is sufficiently controlled. For a round box, checking one nominal diameter and one overall height is rarely enough to understand the structure. Depending on the design, relevant characteristics can include internal diameter, external diameter, body height, lid dimensions, wall build-up, circularity, and the relative alignment of the lid and body.
Routine inspection can use diameter measurements across several orientations and at defined heights to identify meaningful ovalization. Comparing the largest and smallest readings is useful as a production screening method because a cylindrical body can be dimensionally acceptable in one direction while being distorted in another. For projects with tighter geometric requirements, however, this should not be treated as a complete definition of roundness; the measurement method and acceptance criterion need to reflect the actual functional requirement.
The practical importance becomes clear when the lid is fitted. Local distortion may create a tight point, uneven resistance, incomplete seating, or visible tilt even though one diameter measurement falls within specification. A round gift box with lid should therefore have its basic geometry confirmed before opening feel is approved. This also explains why a universal diameter tolerance is not appropriate for every cylindrical package. Diameter, board construction, wrapped material, lid engagement depth, forming method, and intended opening experience all affect how much dimensional variation the structure can tolerate.
Treat Lid-to-Body Fit as a Functional Range
Once the underlying geometry is understood, lid-to-body fit can be evaluated as a functional relationship rather than as a subjective impression from one sample. Commercial production does not need every box to reproduce exactly the same opening force. It needs a controlled range within which the lid can be assembled efficiently, seat fully, remain visually aligned, stay secure during normal handling, and open without excessive force.
The appropriate fit depends on lid depth, dimensional clearance, material friction, package size, wrapped surface, and the experience the brand wants to create. A premium package may intentionally use moderate resistance to create a slower opening action, but that resistance should not deform the cylindrical wall, cause the surface paper to rub excessively, or make opening inconsistent from one orientation to another. Repeated operation can also be relevant for packaging that is intended to remain in use after purchase, because friction and local deformation may change the fit after several opening cycles.
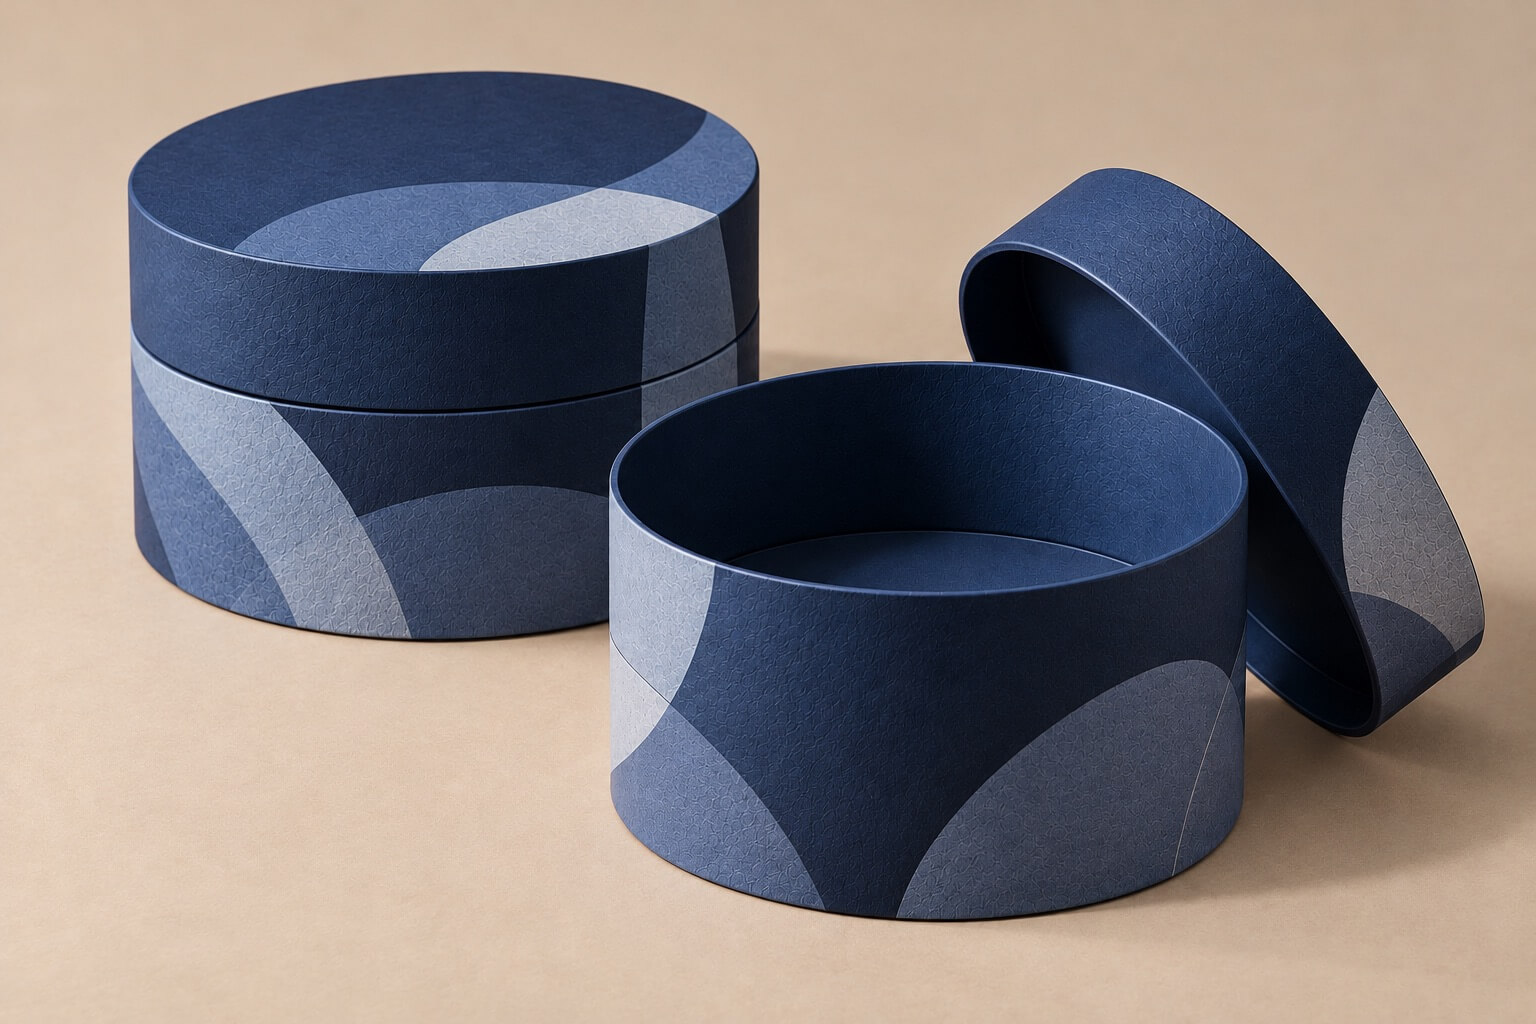
Where production lids and bodies are expected to be interchangeable, cross-pairing samples provides useful information about tolerance interaction. Testing only the original matched pairs can hide a problem if one slightly larger lid happens to be paired with one slightly larger body. Exchanging components between samples helps show whether the intended fit remains acceptable when normal dimensional variation combines differently. This is particularly relevant for rigid boxes custom to a defined specification, because production approval should establish a workable tolerance relationship rather than preserve one fortunate sample pairing.
Validate the Package With the Intended Product and Insert
After the empty structure has passed geometric and functional evaluation, testing should move to the complete packed configuration. Product loading introduces mass, center of gravity, contact points, and internal forces that are absent when the package is evaluated empty. As a result, an empty box can appear stable while the same structure behaves differently once the intended product is installed.
The final product should therefore be used wherever practical, or replaced by a sufficiently representative equivalent during development. The closer the substitute matches the final product in geometry, weight, center of gravity, and contact surfaces, the more useful the result becomes. An empty fragrance bottle, for example, may be suitable for checking cavity dimensions but cannot fully represent the loads created by a filled glass bottle. If the insert provides strong lateral retention but insufficient bottom support, the problem may not become visible until the actual product mass is introduced.
Insert clearance should also be treated as a functional variable rather than simply minimized. Reducing clearance can limit movement, but an excessively tight insert may slow the packing operation, place unwanted pressure on sensitive surfaces, distort paperboard components, or make product removal difficult. The target is controlled retention: enough support to maintain product position through handling without turning the insert into an interference fit that creates new functional problems.
The insert itself cannot be expected to correct every weakness in the outer structure. It can distribute loads, limit movement, and provide local support, but inadequate bottom attachment, unstable wall formation, or weak structural joints remain problems in the outer package. This is why a candle, a glass fragrance bottle, and a multi-product cosmetic set can require different internal engineering even when their external packaging dimensions are similar. Demei’s round rigid gift box for cosmetics provides an example of treating product organization, internal support, and opening structure as parts of the same packaging system.
Follow the Load Path Through the Complete Structure
Once the packed configuration has been established, structural evaluation should consider how forces travel through the package rather than relying on how rigid the box feels in the hand. When a packed cylindrical box is lifted, placed on a surface, pressed laterally, stacked, or subjected to handling shock, the resulting loads can pass through the product, insert, bottom, cylindrical wall, and structural joints in different combinations. The weakest point in that load path can determine performance even when the visible wall itself appears substantial.
Increasing greyboard thickness does not automatically produce a stronger round package. Greater thickness may improve certain stiffness characteristics, but overall structural performance also depends on board properties, package diameter and height, forming accuracy, joint construction, bottom attachment, and internal support. If a relatively heavy product is primarily loading the bottom connection, increasing wall thickness without improving the bottom structure may have little effect on the dominant failure mode. Conversely, a strong outer cylinder does not prevent product movement if the insert provides inadequate restraint.
Structural validation should therefore be connected to credible failure modes. Depending on the product and package design, these may include local sidewall deformation, bottom displacement, joint movement, insert collapse, loss of circularity, or deterioration in lid function after handling. This separates material specification from packaging performance: board thickness is one design input, while structural performance results from how the complete construction manages the actual load.
Approve Printing and Finishing on the Final Construction
Appearance approval becomes more meaningful after the structural configuration has stabilized. A cylindrical surface creates manufacturing conditions that differ from those of a flat carton panel because printed wrapping paper must conform to a curved substrate while maintaining acceptable artwork position, seam appearance, adhesion, and surface smoothness. If the body diameter, wrapping construction, or seam position is still changing, approving decorative details too early can result in a visually approved sample that no longer represents the final structure.
For custom gift boxes with logo wholesale projects, consistency of brand presentation is particularly important. Artwork that is perfectly positioned in the flat file can appear shifted after wrapping because seam position, material behavior, registration, or placement changes around the circumference. Final sample inspection may therefore need to consider color, artwork position, seam location, wrap overlap, foil or emboss registration, surface wrinkles, edge finishing, adhesive contamination, and visible differences around joined areas.
The importance of a visual variation also depends on where it occurs. A minor overlap difference on a concealed rear seam does not have the same commercial impact as an equivalent deviation crossing a front-facing logo or decorative focal point. For this reason, an effective appearance standard should identify critical presentation areas and unacceptable conditions rather than relying only on a general requirement such as “same as sample.” Viewing distance, lighting, orientation, and inspection conditions should also be sufficiently consistent when appearance decisions are commercially important.
Move From Sample Success to Production Repeatability
By this stage, the sample may have acceptable geometry, lid fit, product support, structural behavior, and surface appearance. The approval question now changes. The manufacturer has demonstrated that the package can be made successfully; the next task is to establish whether the characteristics responsible for that result can be maintained with sufficient consistency when production volume increases.
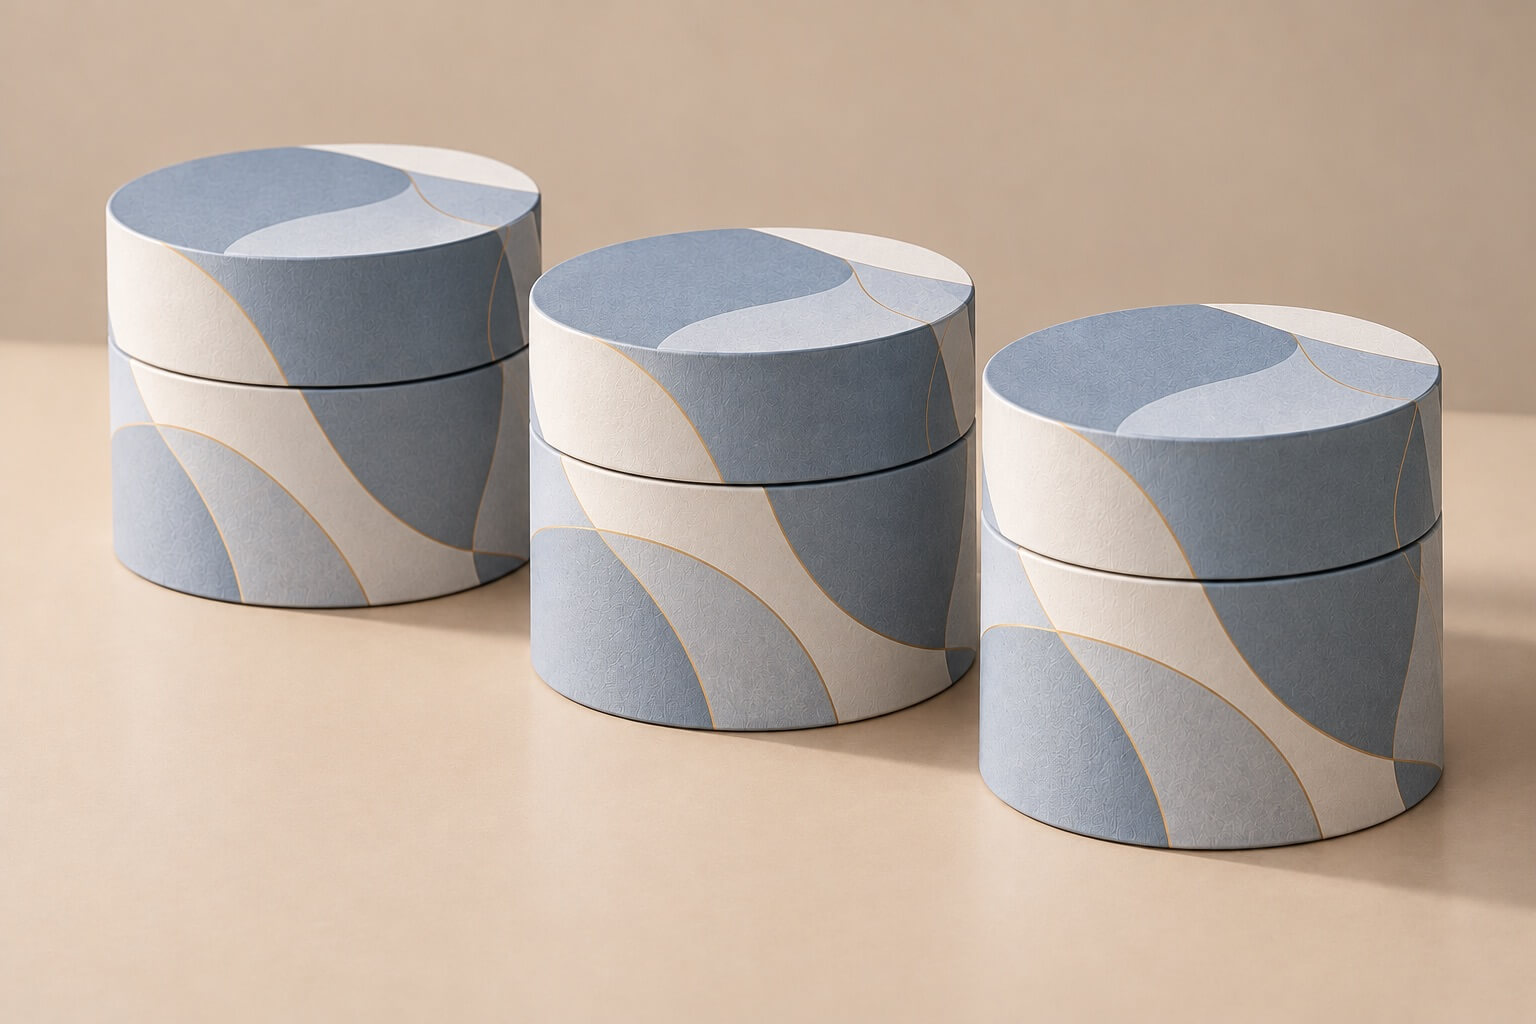
There is no technically responsible universal number of samples that proves a package is ready for production. The appropriate sampling approach depends on order size, process maturity, project risk, critical characteristics, manufacturing history, and what the evaluation is intended to demonstrate. A small group of samples can reveal obvious variation, but it does not automatically demonstrate statistical process capability. Projects with tighter dimensional or functional requirements may justify a production trial, defined sampling plan, measurement records, or additional process controls before full release.
This is also an important distinction when comparing rigid box suppliers. Producing one high-quality sample demonstrates development capability; explaining how critical characteristics will be controlled demonstrates production capability. For cylindrical packaging, relevant characteristics may include diameter variation, lid-to-body fit, body height, seam position, bottom integrity, insert location, and finishing registration. These characteristics do not all require the same inspection frequency, but those with a meaningful effect on function, appearance, or product protection should have a defined control method.
Mass-produced units should consequently be judged against the approved specification and acceptance criteria rather than against the unrealistic expectation that every unit will be physically identical to one handcrafted sample. Manufacturing inevitably contains variation; professional quality control defines which variation is acceptable, measures the characteristics that matter, and establishes action when those limits are exceeded.
Validate the Complete Packed System for Distribution
After production repeatability has been considered, physical validation should reflect the conditions under which the product will actually move through the supply chain. The relevant test unit is not simply the decorative package. It is the complete packed system: product, insert, presentation package, protective components, shipping carton, and actual packing arrangement. A decorative circle gift box intended mainly for controlled retail handling may face different risks from a package distributed through multiple warehouses, parcel networks, or international freight routes. Although consumers may search for gift boxes round, the manufacturing specification has to account for the physical conditions those boxes experience before reaching the consumer.
A successful drop test alone does not establish that a package is suitable for every shipping environment. Distribution can expose the packed system to shock, vibration, compression, repeated handling, and environmental changes, and these hazards interact differently with different products and packing configurations. Validation should therefore reflect the intended logistics system. Where appropriate, recognized packaged-product testing procedures can provide a structured framework, but the selected test sequence and severity should correspond to the product and shipment configuration rather than being treated as a universal certification.
Post-test inspection is as important as performing the test itself. The package should be reassessed against the characteristics established earlier: whether the body remains acceptably round, whether the lid still seats and opens correctly, whether the bottom and structural joints remain stable, whether the insert still retains the product, and whether abrasion or movement has damaged the finished surface. Product damage and unacceptable internal movement should also be evaluated. This closes the validation loop because the objective is not simply for the package to remain intact; it is for the functions approved before distribution testing to remain acceptable afterward.
For brands manufacturing in Asia and supplying North America, Europe, the Middle East, or other international markets, shipment method, master-carton configuration, handling system, storage environment, product mass, and packing density are generally more useful engineering inputs than destination names alone. If the logistics configuration changes materially after approval, the relevance of the original distribution validation should be reviewed rather than assumed.
Convert Approval Into a Controlled Production Standard
The final stage is to translate validated performance into information that production and quality teams can actually control. A physical approved sample remains valuable because it communicates the agreed construction, appearance, and overall presentation, but it cannot precisely define every dimensional tolerance, material requirement, test method, artwork revision, or acceptance limit.
A Golden Sample should therefore function as a physical reference within a broader approval system rather than as the entire production standard. It is most useful when linked to controlled structural drawings, material specifications, artwork files, finishing requirements, critical dimensions, functional acceptance criteria, and packing instructions. If the physical reference and written specification appear to conflict, the approval documentation should identify which requirement governs instead of leaving the decision to individual interpretation on the production floor.
This level of definition also improves supplier comparison. Broad commercial descriptions such as box rigid can be useful at the beginning of sourcing, but they do not establish a manufacturing specification. Two quotations for apparently similar cylindrical boxes may assume different board constructions, insert materials, wrapping methods, dimensions, finishing tolerances, or inspection standards. Without a controlled specification, the prices may look directly comparable even though the underlying packages are technically different. Demei’s packaging FAQ provides additional context on sampling and production, while its production and quality control approach explains the broader transition from packaging development into manufacturing.
Before production release, the brand and manufacturer should also identify which changes would invalidate part of the earlier approval. A change in board construction, product weight, insert geometry, critical dimensions, finishing process, or shipping configuration can alter the relationships that were previously tested. Production approval should therefore follow the specification and configuration that were validated, not simply the product name or visual appearance of an earlier sample.
Conclusion: Approve a Reproducible Packaging System
Pre-production testing is not intended to prove that one attractive sample can be made. Its purpose is to establish sufficient evidence that the intended packaging system can be manufactured, packed, handled, and distributed within defined requirements. That evidence develops progressively: the specification establishes what is being evaluated; geometry confirms whether the components have the intended form; functional testing determines whether those components work together; packed-product testing introduces actual loads and interactions; and structural and surface evaluation determines whether performance and presentation remain acceptable.
Repeatability then establishes whether the critical results can be controlled across production, while distribution validation determines whether those approved characteristics remain acceptable after realistic handling. Once these relationships are documented, the approved physical sample becomes part of a much stronger production standard rather than the sole definition of quality.
For brands ordering cylindrical packaging, this approach creates a more reliable basis for mass-production approval than appearance alone. It turns sample sign-off into a controlled transition between packaging development and repeatable manufacturing.