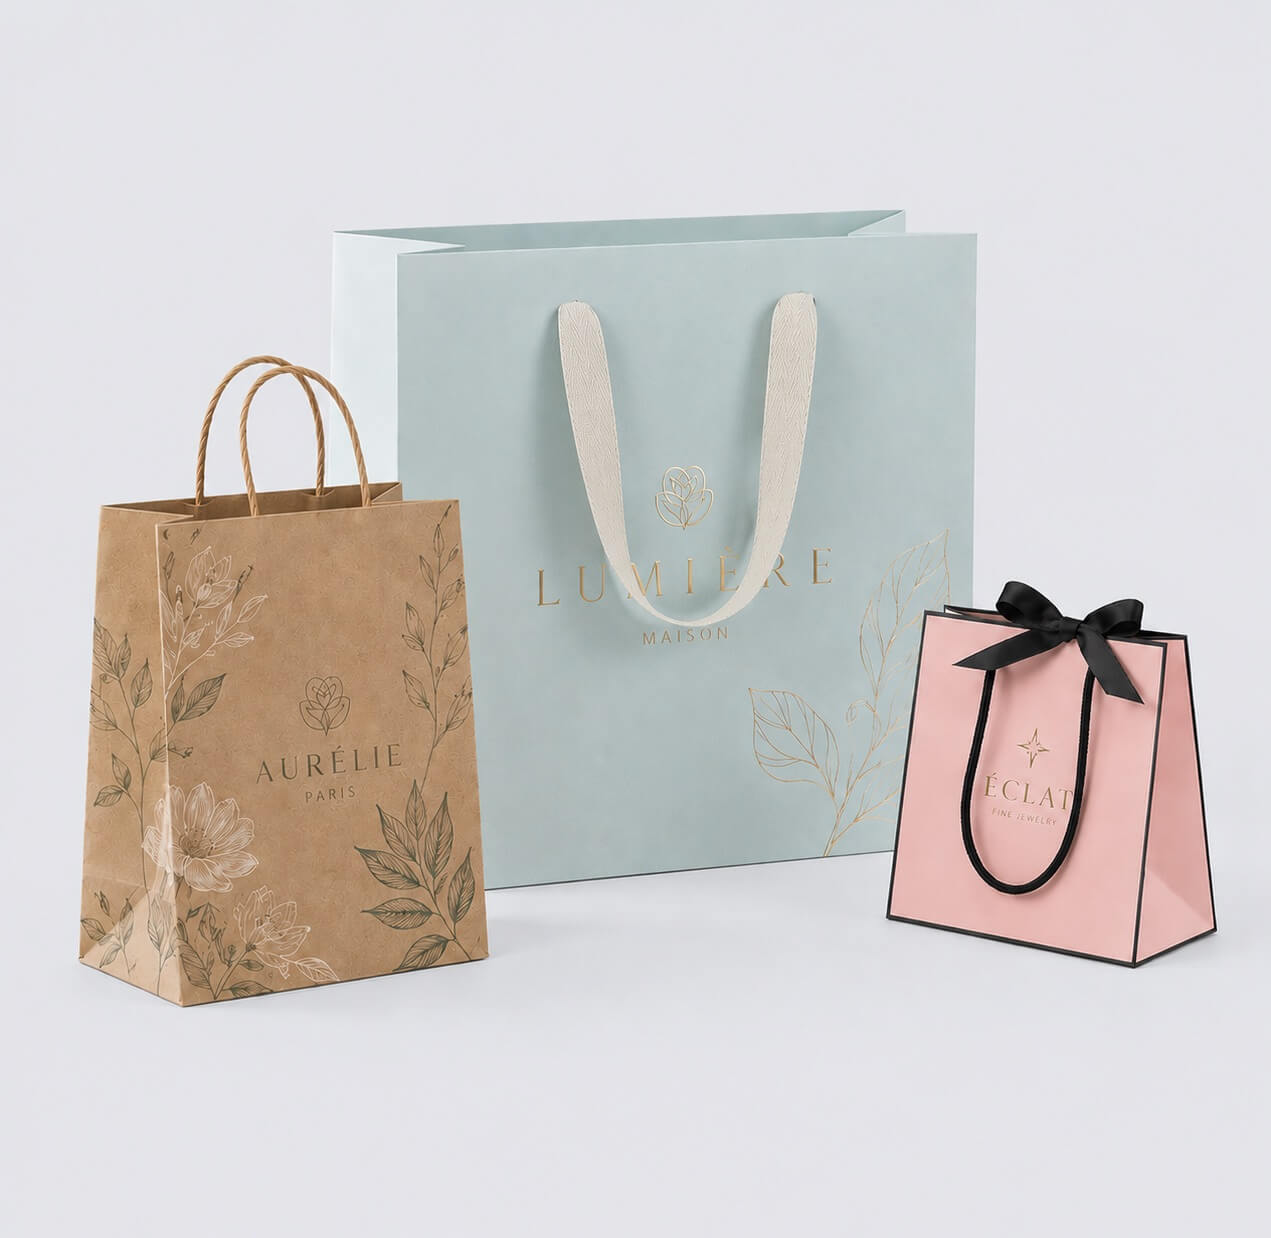
A paper shopping bag can provide sufficient internal capacity while remaining difficult to use during retail packing. The product may fit comfortably once positioned at the bottom, yet the employee may still need to widen the opening, reposition the handles, rotate the merchandise, or stabilize the bag during insertion. These difficulties occur because the space available inside a finished bag is not necessarily the same as the space accessible throughout the packing operation.
For brands developing custom made shopping bags, this distinction changes how packaging performance should be evaluated. Rather than treating the finished dimensions as the primary measure of suitability, the design process should examine how the structure behaves during opening, loading, arrangement, and handover. This approach is particularly relevant to custom gift paper bags carrying rigid presentation boxes and custom kraft shopping bags used in high-frequency retail transactions, where differences in merchandise geometry and operator movements can produce different functional requirements.
Effective retail packaging therefore requires coordination between product characteristics, bag construction, and the intended packing sequence. As part of professional packaging design and engineering, the objective is not simply to create a container with adequate capacity, but to develop a structure that allows merchandise to be loaded predictably without unnecessary deformation, repeated manipulation, or avoidable product contact.
Why Must Retail Packing Operations Be Defined Before Bag Geometry?
The starting point for operational packaging design is the packing task rather than the bag itself. A beauty retailer placing several boxed cosmetics into one shopping bag encounters different handling conditions from a fragrance boutique loading a single presentation box. Apparel retailers may handle products that compress or change shape, while stores selling candles or glass containers must manage rigid products whose orientation and contact conditions are more restrictive.
These differences establish distinct operational requirements. Before developing the bag structure, brands should identify the representative product combinations, their preferred loading orientations, and the sequence in which employees normally handle them. Counter height, available working space, bag storage position, and whether the employee can use both hands also influence the operation. A design that requires continuous manual support may work at a spacious packing station but become inconvenient where one hand must remain available for scanning, wrapping, or arranging merchandise.
The packing process can be treated as a sequence of connected states: the bag is retrieved in a flattened condition, opened, positioned on the counter, loaded, adjusted if necessary, and finally lifted for handover. Each transition introduces a possible operational constraint. If the bag cannot remain sufficiently open, loading becomes more difficult. If merchandise must be rotated during insertion, the opening must accommodate that movement. If the contents are unstable before lifting, the handover stage may require additional adjustment.
Does choosing a larger shopping bag automatically improve packing efficiency? No. Additional internal space may reduce some product-clearance problems, but it can also permit uncontrolled movement or require more repositioning during loading. The appropriate geometry depends on how the merchandise enters and occupies the bag, not simply on whether its dimensions are smaller than the stated internal capacity.
Once the packing task is defined, the next question is whether the bag can establish and maintain the opening required to begin that task.
How Does Opening Geometry Change During the Packing Process?
Unlike a rigid container, a conventional paper shopping bag does not maintain one fixed three-dimensional geometry throughout handling. When stored flat, the side gussets are folded inward and the bottom construction is collapsed. Opening the bag requires these folded regions to rotate, unfold, and develop into a usable interior space. The resulting configuration depends on crease behavior, panel stiffness, residual deformation from storage, and the interaction between adjacent panels.
This creates an important distinction between nominal bag dimensions and effective opening geometry. A bag may be specified by width, gusset depth, and height, but those measurements do not establish the accessible area at every stage of opening. The entrance can remain restricted by partially unfolded gussets, inward-moving upper corners, or handles crossing the loading area. Its effective shape may also change as the operator releases the bag or inserts the first product.
For premium paper bags carrying relatively rigid merchandise, this distinction can be significant. A stiff upper section may help preserve the intended appearance, but it can also resist temporary deformation when a product passes through the opening. Conversely, flexible panels may expand readily while providing insufficient stability to maintain the entrance without manual support. Neither characteristic is automatically preferable; the correct balance depends on the loading operation.
Why can a bag with adequate internal dimensions still be difficult to open and fill? Because the accessible opening is a temporary structural condition, not simply a dimension printed on the specification sheet. Two bags with similar finished dimensions may behave differently if their gusset geometry, crease formation, or upper-edge construction affects how the opening develops.
During prototype evaluation, opening performance should therefore be assessed under defined conditions. The reviewer should record whether the bag opens with the intended hand movements, whether the base unfolds correctly, and whether the entrance remains accessible long enough to begin loading. These observations establish the functional starting condition for evaluating product insertion.
Why Is the Product Insertion Envelope Different From Final Internal Clearance?
Once the bag can be opened reliably, the central geometric problem becomes the path followed by the product. The final packed position describes where the merchandise rests after loading; the insertion envelope describes the space it occupies while moving toward that position. These are different conditions, especially when the product must be tilted, rotated, or guided past the bag’s upper structure.
Consider a rectangular fragrance gift box. When lowered vertically, its corners follow a relatively direct path into the bag. If the box must be tilted to clear the entrance, its projected dimensions relative to the opening change during rotation. A diagonal corner may approach the side panel even when the box’s final footprint is smaller than the internal base dimensions. The amount of clearance required therefore depends on the complete movement, not merely on the product’s length, width, and height.
This interaction becomes more complex when the merchandise has projecting lids, decorative closures, or surfaces vulnerable to abrasion. A rigid edge contacting an inward-folded gusset may temporarily push the panel out of position, while a projecting component may catch near the upper reinforcement. Such contact does not necessarily indicate that the bag is undersized; it may indicate that its opening geometry is incompatible with the intended loading orientation.
For customized paper gift bags, a practical evaluation should use the actual packaged product or a dimensionally representative model that reproduces relevant projections and contact surfaces. A plain rectangular block cannot fully represent the insertion behavior of a package with an overhanging lid.
How much clearance should be allowed between the product and the bag opening? There is no universal clearance suitable for every construction. The requirement depends on product geometry, loading orientation, allowable contact, bag deformation, and operator variability. A clearance that works for a smooth rectangular package may be insufficient for merchandise with projecting corners or delicate finishes.
The appropriate engineering method is to establish a feasible insertion path, identify its most restrictive positions, and verify that the product can pass through them without excessive force or unacceptable contact. Once this path is confirmed for a single item, the design must be evaluated under the more complicated conditions created by multiple products.
How Do Product Combinations Change Packing Geometry and Stability?
Multi-item packing is not equivalent to placing several independently compatible products into the same container. Each item changes the available space and may restrict the insertion path of the next. The sequence also influences how loads are distributed through the bag bottom and whether the contents remain stable while the operator prepares for handover.
Consider a retail purchase containing a cylindrical skincare bottle, a rectangular cosmetic carton, and a smaller accessory. If the bottle is loaded first and placed centrally, it may obstruct the path required for the carton. If the carton is loaded first, its flat surface may provide a useful positioning reference, but the remaining space may not accommodate the bottle in its intended orientation. The practical solution depends on the dimensions, rigidity, surface sensitivity, and relative positions of the products.
Should heavier merchandise always be loaded first? Not necessarily. Although placing heavier products lower in the bag can improve stability and reduce compression of lighter items, weight alone does not determine the correct sequence. A narrow, heavy bottle may remain unstable without lateral support, while a relatively light but wide package may establish a more reliable base arrangement. The operator must consider both the final load distribution and the path required to achieve that arrangement.
For personalized paper bags used across product collections, testing only the largest individual product is therefore insufficient. Representative combinations should include purchases that create different geometric constraints, such as one large rigid item, several small items, and mixed-height products. The purpose is not to reproduce every possible retail transaction, but to identify combinations that challenge the opening, internal arrangement, and transfer process in different ways.
The distinction between an occasional adjustment and a systematic design problem is important. If several operators repeatedly encounter the same interference at the same stage, the issue may originate from the packaging configuration rather than individual packing technique. That observation should lead to a structural review before additional operating instructions are introduced.
How Do Handles, Upper Reinforcement, and Counter Support Interact?
After the loading arrangement is established, the complete process must also account for how the bag is supported and handled. During packing, the bottom panel transfers the weight of the merchandise to the counter. During lifting, the load path changes as the handles carry the suspended weight through their attachment regions and the bag body. The transition can cause the contents to settle or shift, particularly when the arrangement is asymmetrical.
Handle construction affects this transition, but its operational influence begins before lifting. Long handles may fall across the opening while products are inserted, while upper reinforcement can restrict local movement near the entrance. A handle design may therefore satisfy its carrying requirement yet still interfere with merchandise loading. Similarly, a bag that stands adequately when filled may collapse when empty or partially loaded, requiring the employee to hold the entrance open.
For custom printed paper shopping bags, decorative elements should be assessed within this functional context. The purpose is not to reduce visual quality, but to ensure that handle placement and upper-edge construction do not create avoidable interference during routine use. The same principle applies when comparing different retail packaging options, where structural differences can affect product presentation and handling.
Can a bag pass a handle-strength test and still perform poorly during retail packing? Yes. Handle strength evaluates resistance to a specified load or loading condition, whereas packing usability concerns accessibility, manipulation, and the transition from counter support to carrying. Passing one assessment does not establish satisfactory performance in the other.
A complete functional trial should therefore include empty-bag opening, partial loading, full loading, handle retrieval, initial lifting, and controlled handover. The observations should distinguish product movement caused by the lifting transition from interference occurring earlier during insertion.
These findings provide the basis for evaluating the packing process systematically rather than relying on subjective impressions of convenience.
How Can Packing Performance Be Evaluated Through Controlled Trials?
Operational validation requires more than demonstrating that one experienced employee can fill a selected prototype. A credible comparison should control the main variables affecting the task so that differences between bag designs can be interpreted meaningfully.
The test should define the product combination, loading sequence, counter arrangement, initial bag condition, and operator instructions. For comparative trials, the same merchandise and operating conditions should be used across candidate structures. Because operator familiarity influences performance, repeated observations involving more than one operator can help distinguish design-related constraints from individual technique.
Evaluation should include both measurable results and structured observations. Useful indicators include opening time, total packing time, corrective hand movements, product repositioning events, unintended contact with bag surfaces, and successful completion of the prescribed loading sequence. These measures should not be combined into an arbitrary performance score unless the evaluation method and relative importance of each criterion have been defined in advance.
Is the fastest packing design necessarily the best? No. A structure that reduces loading time but increases product abrasion, instability, or handling errors may be unsuitable. Packing efficiency should be considered alongside functional reliability and product protection.
A further distinction is required between repeatability and isolated success. One successful loading attempt demonstrates feasibility under that particular condition. It does not establish that the same operation will remain reliable across different operators, representative product combinations, or reasonable variations in the bag’s manufactured condition.
A practical development process can therefore begin with screening trials to identify major interference, followed by more structured confirmation of the selected construction. The number of repetitions and acceptance criteria should reflect the operational risk and observed variability rather than an unsupported universal rule.
For projects involving custom printing paper bags, this evaluation complements artwork and appearance approval by addressing functional characteristics that cannot be assessed from a flat printed proof.
Once the trial identifies recurring constraints, the next task is to determine which observations can be converted into controlled design and manufacturing requirements.
How Should Operational Findings Be Converted Into Manufacturing Specifications?
The most important outcome of functional testing is not a statement that one prototype is easier to use. It is a clear relationship between an observed problem, its probable structural cause, and a requirement that can be verified.
For example, repeated difficulty opening the bag may involve crease geometry, side-gusset recovery, or deformation caused by storage compression. Product interference near the entrance may originate from upper-edge construction, gusset intrusion, or insufficient working clearance. Unstable loading may involve the relationship between bottom geometry and the product arrangement. Each observation requires a different technical response.
A useful engineering approach separates three levels of control. The first is the functional requirement, such as allowing a defined reference product to pass through the opening without forced deformation. The second is the design characteristic believed to influence that function, such as opening geometry, gusset configuration, or handle position. The third is the manufacturing characteristic that must be controlled to maintain the approved design, such as cutting dimensions, crease placement, folding accuracy, or assembly alignment.
These levels should not be confused. Measuring a crease position accurately does not, by itself, prove that the finished bag opens correctly. Likewise, a successful loading trial does not establish that every production unit will reproduce the same behavior. Dimensional inspection and functional validation provide different forms of evidence and should be used together where appropriate.
What should brands specify if opening performance cannot be represented by one dimension? They can define a reference bag condition, a representative loading product, an agreed operating procedure, and observable acceptance criteria. The manufacturer can then identify which production variables are critical to achieving the required function.
When developing custom retail packaging, brands should translate these operational findings into measurable structural and manufacturing requirements rather than leaving them as subjective feedback.
The final design review should confirm that these requirements are practical to manufacture and that the selected verification methods correspond to the actual operational risks.
What Defines a Production-Ready Retail Packing Design?
A production-ready shopping bag should demonstrate more than successful product fit or an acceptable appearance. It should support the complete intended sequence, from opening and loading to lifting and handover, under defined and representative conditions.
The approval process should therefore confirm which product combinations have been evaluated, which loading orientations are acceptable, what adjustments operators are permitted to make, and which forms of interference or deformation are unacceptable. These requirements establish the intended operating boundaries of the design. They also help prevent a prototype from being approved solely because a particular operator was able to compensate for its limitations.
For international retail programs, documented requirements become particularly useful when the same bag is supplied to stores with different employees, counter arrangements, and merchandise combinations. However, the relevant conditions must still be defined for each application; a successful test in one store configuration does not automatically establish suitability for every retail environment.
Physical sampling remains an important part of this process, but the sample should be evaluated against agreed functional requirements rather than appearance alone. Demei’s sampling and production guidance provides further information about the development and manufacturing process.
Ultimately, engineering a shopping bag around retail packing operations means treating the bag and the packing procedure as one functional system. Opening geometry establishes access, insertion paths determine movement, product arrangements influence stability, and handle behavior affects the final transfer. Functional testing connects these interactions, while manufacturing specifications establish the characteristics needed to reproduce the approved design.
A successful result is not simply a bag large enough to hold the merchandise. It is a structure that allows the intended retail packing operation to be performed consistently, with controlled handling, acceptable product contact, and clearly defined performance requirements.